
Lithium Ion Battery Recycling Solutions for Black Mass Recovery
With the rapid development of new energy vehicles and consumer electronics, the usage of lithium-ion batteries is constantly increasing, leading to the generation of vast quantities of end-of-life batteries. To facilitate resource recycling, specialized lithium battery recycling equipment has become a critical component in the industry's development. Through a comprehensive suite of automated equipment and process workflows, SUNY GROUP enables the safe and efficient separation of valuable materials from lithium batteries, while simultaneously enhancing the recovery rate and purity of "Black Mass."
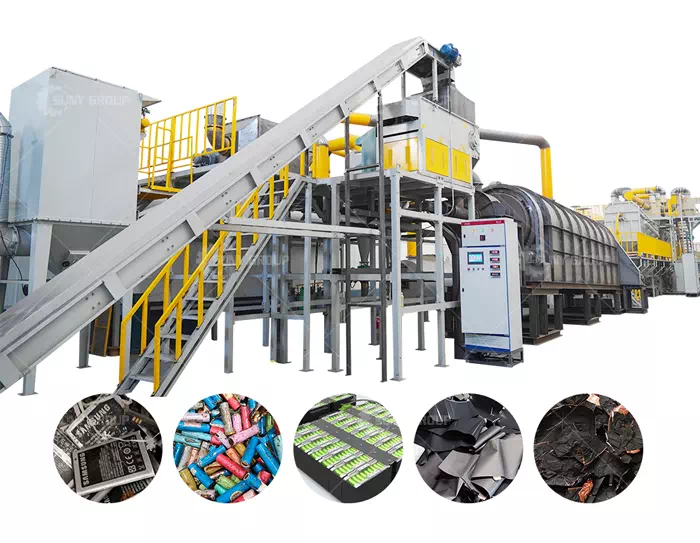
Nitrogen-Protected Crushing and High-Temperature Thermal Treatment System
Safety is a paramount concern throughout the lithium battery recycling process. This recycling production line begins with a nitrogen-protected crushing system, which processes waste lithium batteries within an inert gas environment to mitigate the risk of combustion or explosion during the crushing phase.
Following the crushing stage, the material enters a high-temperature pyrolysis system for further processing. This high-temperature pyrolysis technique effectively eliminates electrolytes and causes the internal structural components of the batteries to loosen, thereby creating optimal conditions for the subsequent separation of Black Mass. This specific stage not only boosts the efficiency of Black Mass release but also contributes to the stable and reliable operation of the downstream sorting equipment.
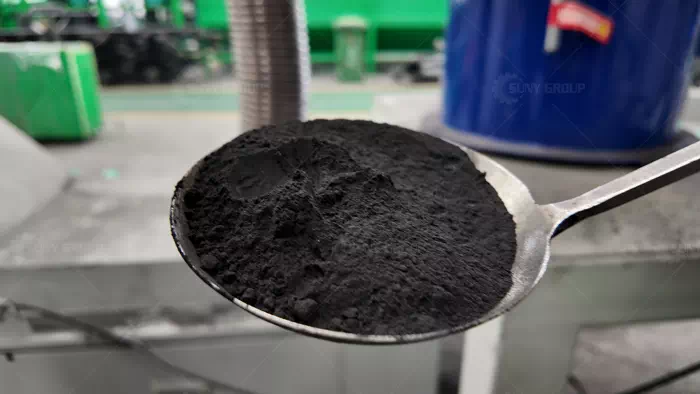
Multi-Stage Sorting Equipment for Enhanced Black Mass Recovery
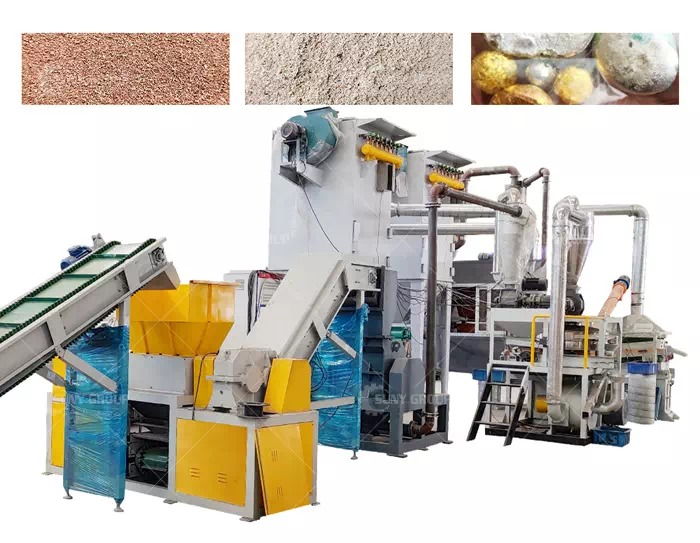
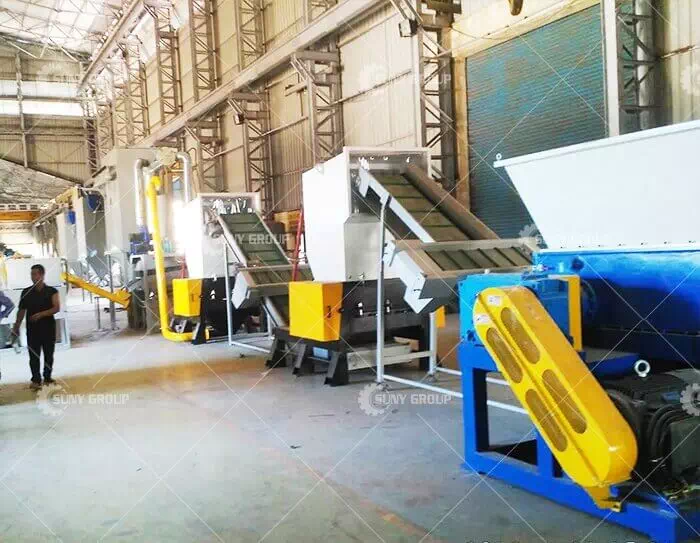
After undergoing thermal treatment, the material proceeds to the sorting phase. Initially, a preliminary separation of casing materials and certain metal components is achieved using zigzag separators and magnetic separation equipment. Subsequently, the material is fed into a hammer crusher for further pulverization, ensuring the more complete liberation of the battery's constituent materials.
To maximize Black Mass recovery efficiency, the production line is also equipped with a dual-roller powder separation unit, designed to further isolate the Black Mass from the battery electrode sheets. Testing has demonstrated that this integrated system can achieve a Black Mass recovery rate of approximately 95%, while attaining a purity level of around 98%, thereby significantly enhancing the economic value of the recovered materials.
In the final stage, airflow sorting equipment is utilized to separate copper and aluminum components, yielding distinct categories of recycled metal resources.
Comprehensive Environmental Protection and Waste Gas Treatment Systems
Environmental management systems play an equally vital role throughout the entire lithium battery recycling production line. The facility is outfitted with a complete waste gas treatment apparatus—including spray towers, dust collectors, and UV photocatalytic oxidation units—designed to effectively process the dust and gaseous emissions generated during the production process. These eco-friendly systems effectively reduce pollutant emissions, ensuring that the entire production process is safer and more environmentally sound. Concurrently, they provide enterprises with a more stable production environment, thereby enhancing the long-term operational reliability of the equipment.
Overall, this lithium-ion battery recycling solution—utilizing a combination of crushing, pyrolysis, and multi-stage sorting equipment—achieves the efficient recovery of materials such as "black mass," copper, and aluminum. It thus offers a mature and reliable technical solution for the resource utilization of waste lithium batteries.
Recommend products
CONTACT US:
If you have any requirement or suggestion, please fill in the form and send to us, thanks!E-mail:[email protected] | Whatsapp:+8613674945231